Equipment & Process
See how our manufacturing partner handles design, machining, assembly, trials and inspection. The equipment and process ranges below describe the workshop supporting your project.
Mold Design in UG / CAD
Every mold begins with design work in Siemens NX / UG, with 2D drawings in AutoCAD. The workshop engineers review manufacturability, parting, gating, ejection and cooling before machining starts.
- DFM review before quote confirmation
- Parting line, gate location and gate type (side / submarine / pin-point)
- Ejection plan — pin, blade, sleeve, lifter
- Cooling plan — line diameter, baffles, spiral cooling where needed
- Slider and lifter design, angle and travel
- Buyer sign-off on 3D mold layout before machining starts
Supported by Long-Term Partners
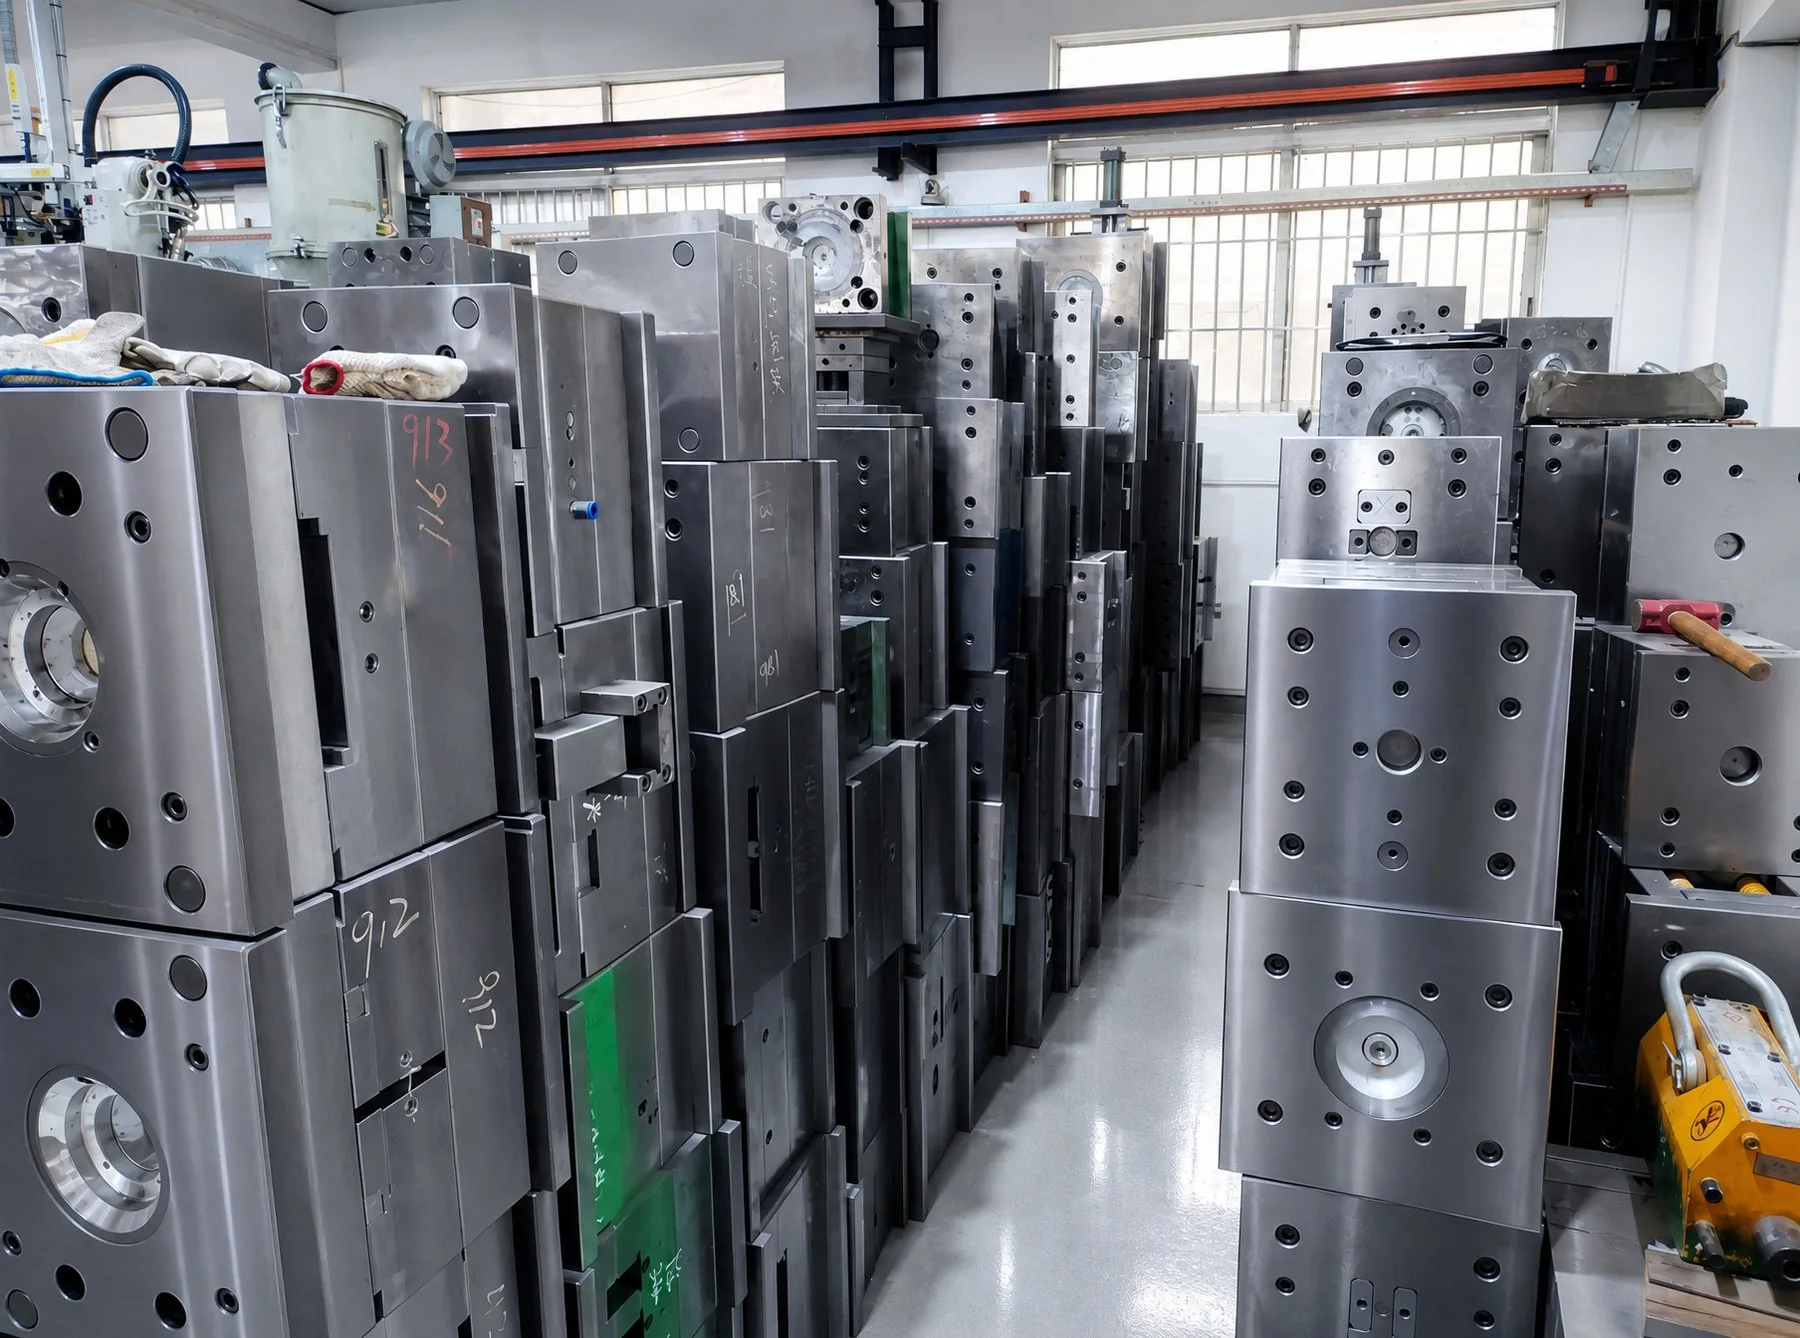
CNC machining is supported by long-term machining partners under our process and quality control. These are shops we have worked with for years — not a random subcontractor for each job.
- CAM programming reviewed by the tooling engineers
- Tool paths agreed for critical surfaces before cutting
- Every returned part inspected against the drawing before fitting
- Traceable material and heat treatment records
EDM, Fitting and Assembly at the Workshop
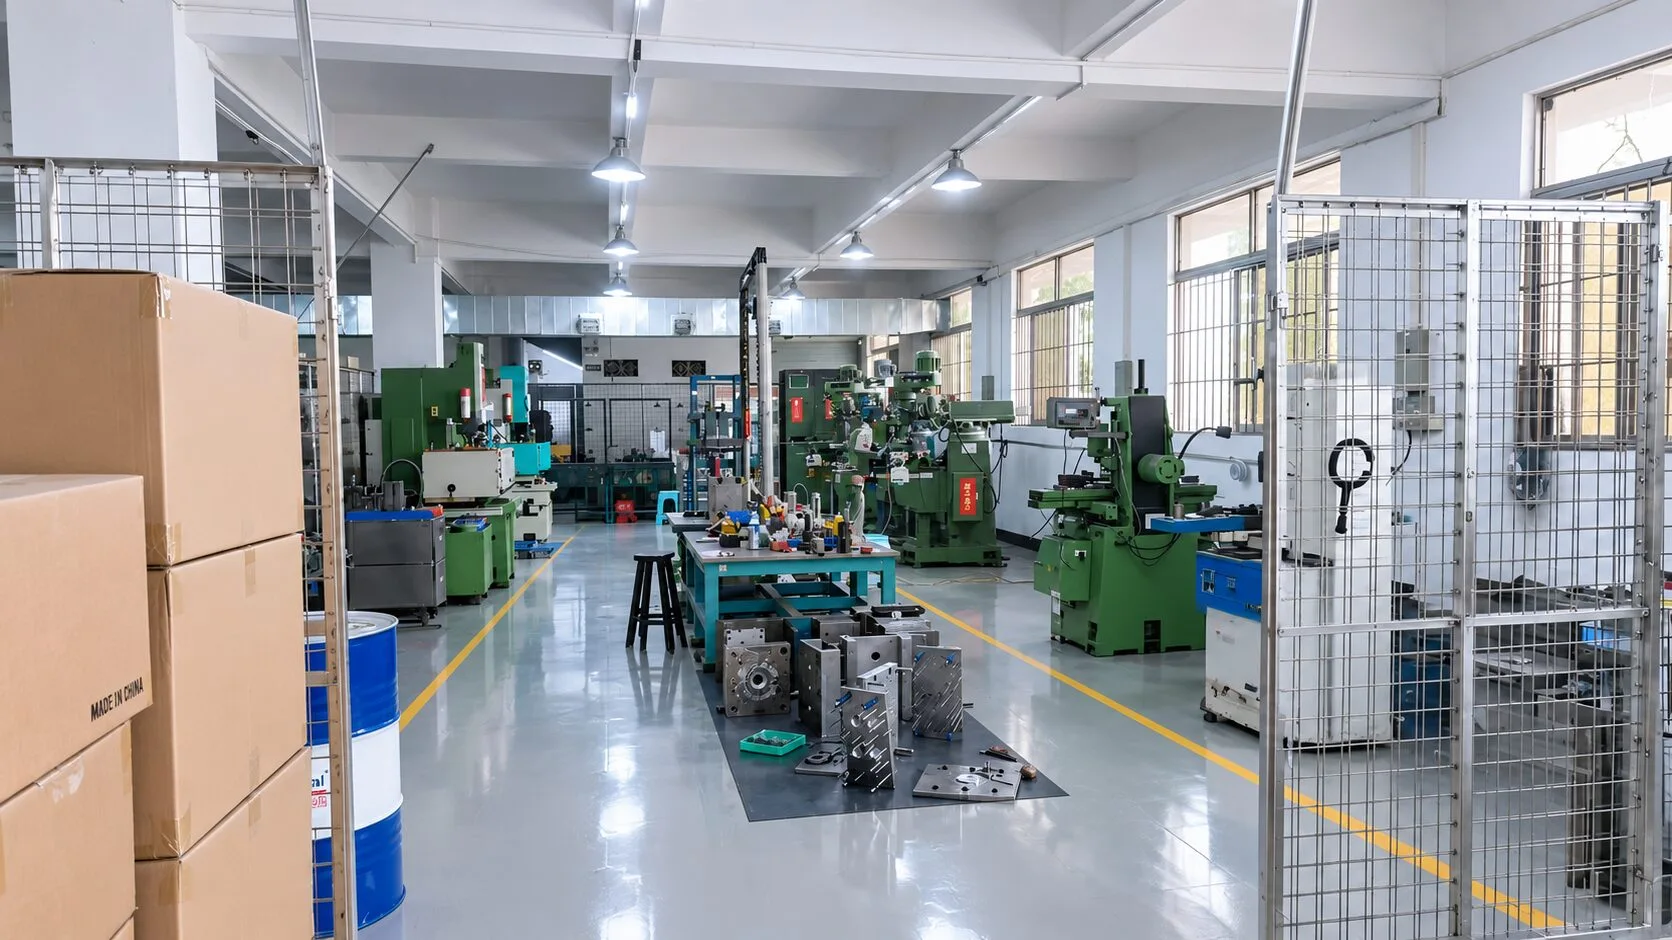
The steps that most affect mold life and part quality are all at the tooling workshop. This is where 25 years of workshop experience actually shows.
- Sinker EDM — ribs, sharp corners, logos, text
- Wire EDM — ejector holes, precision slots, inserts
- Fitting — parting line, shut-offs, slider faces by hand
- Assembly — mold base + core + cavity + slider + lifter + ejector + cooling
- Polishing — from SPI-A3 to optical polish for PC / PMMA lenses
- Correction after T1 — welding, re-cutting, insert changes as needed
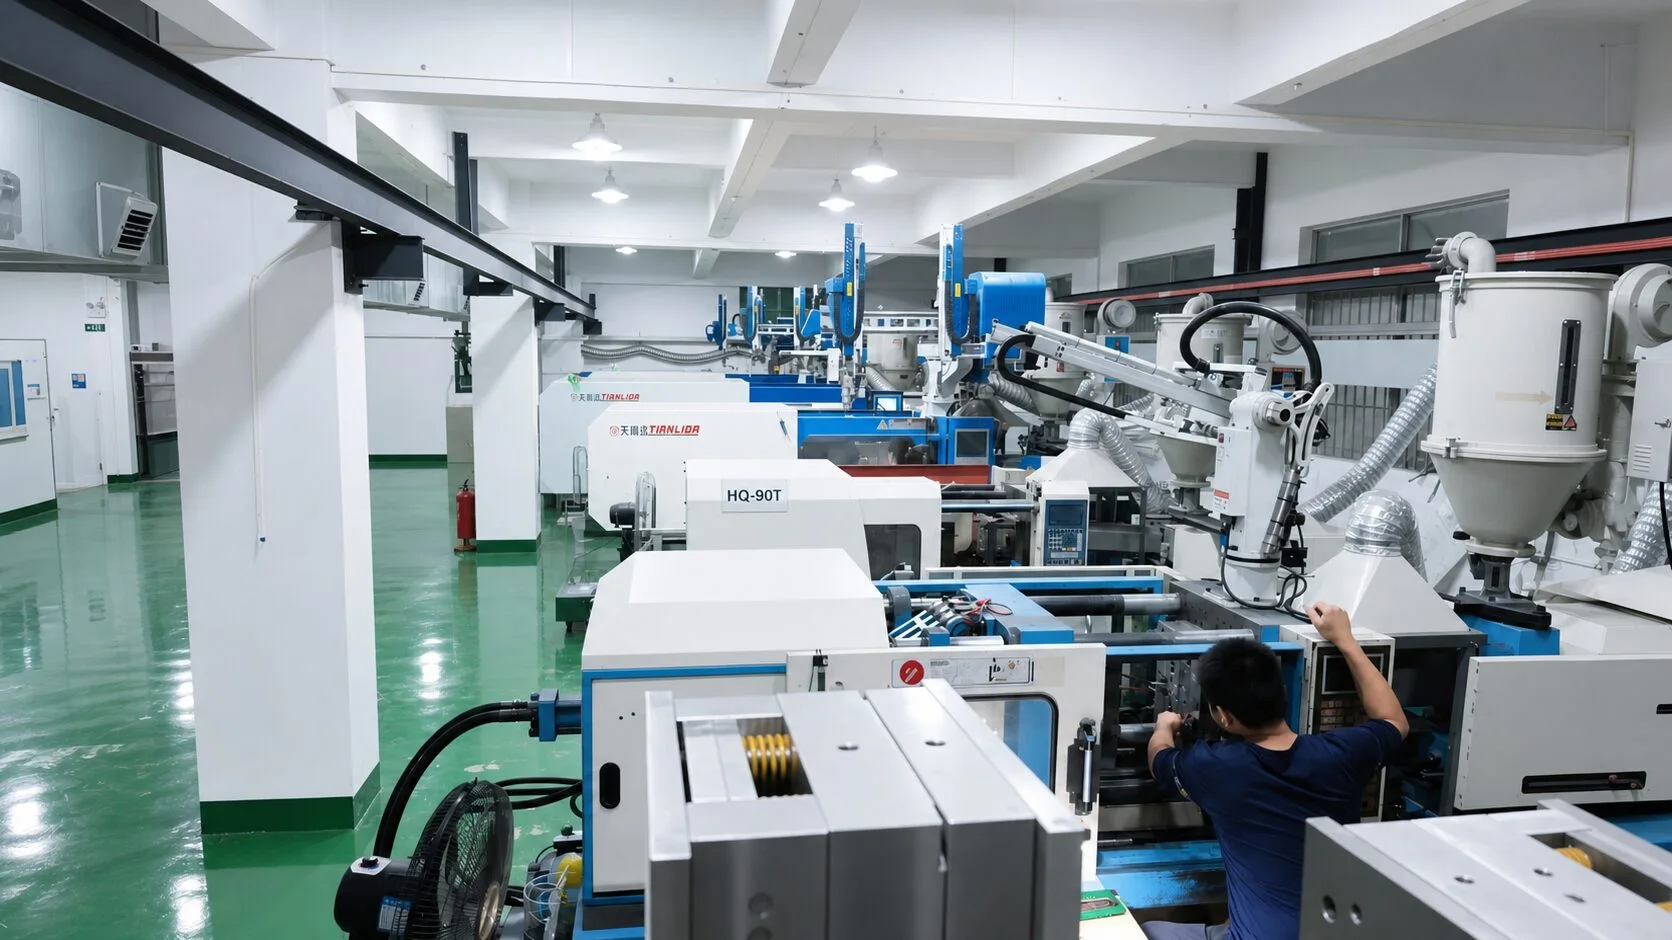
90T – 200T Trial Molding at the Workshop
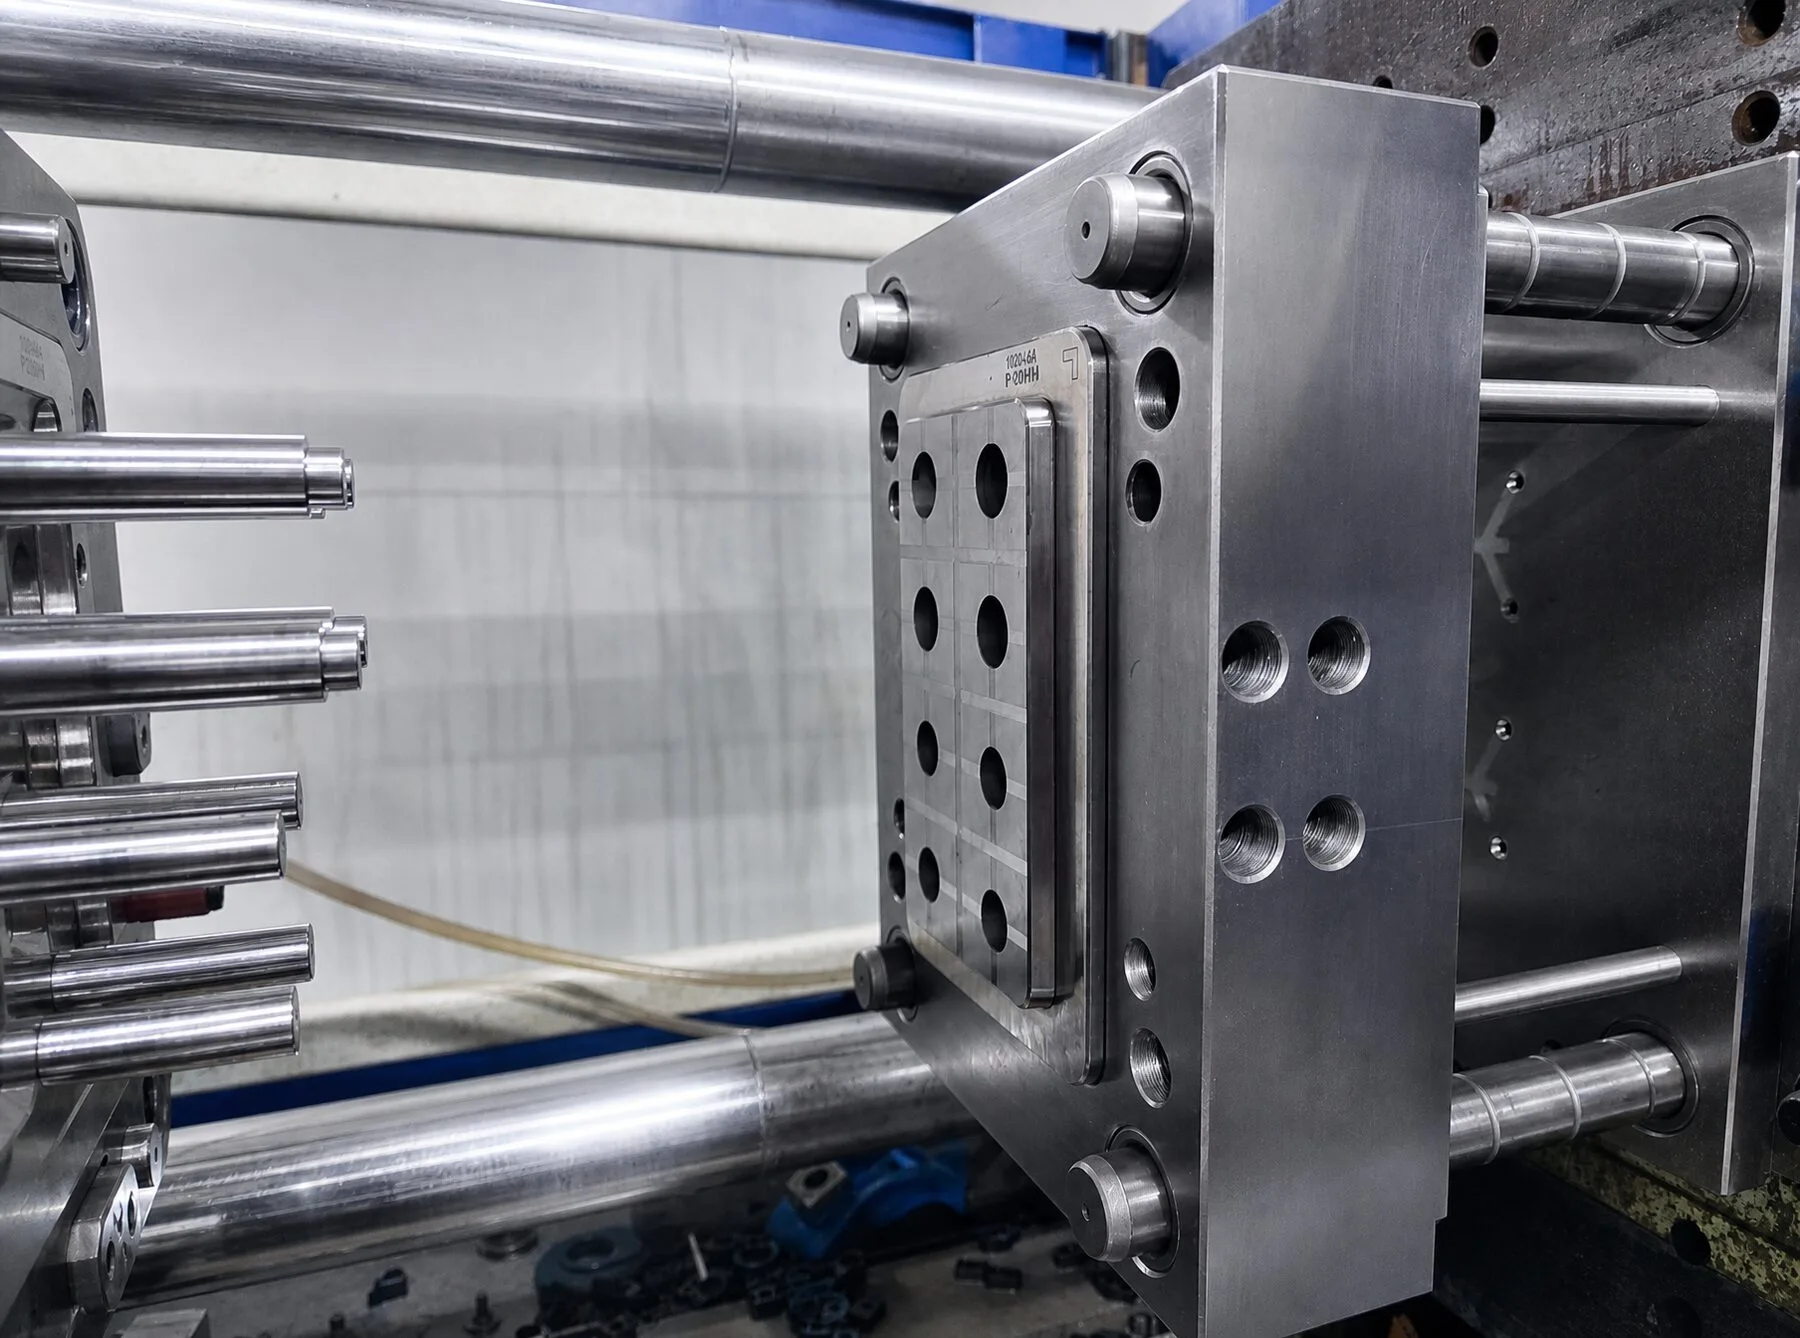
Every mold is tried at the tooling workshop before it ships. The production line covers 90-ton to 200-ton machines, matched to the mold size we build. Robots handle unloading on the machines where they are useful.
- T1 first-shot trial with process record
- Trial video showing mold opening, ejection, part release
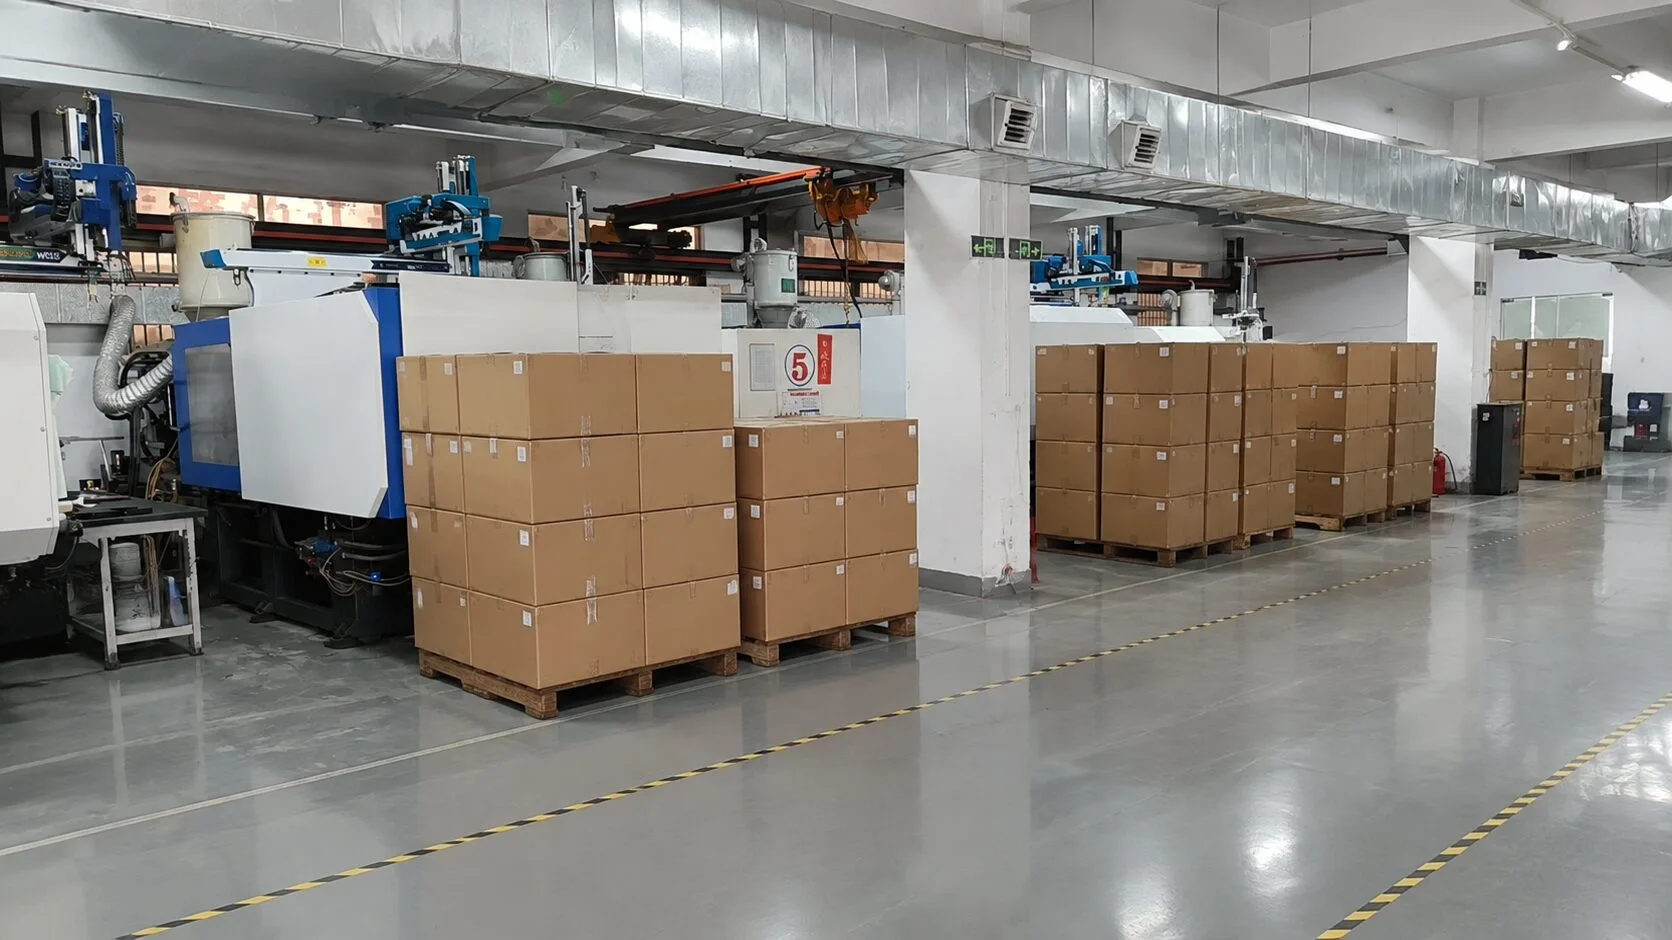
- Sample parts labeled and packed with the tool
- T2 / T3 trials after corrections when needed
- Buyer sign-off on samples before shipment
Documented, Not Assumed
Inspection happens at three points: on machined parts before fitting, on the assembled mold before T1, and on trial parts before shipment. The paperwork ships with the tool.
- CMM inspection of critical part dimensions
- Cavity and core dimensional check against 3D reference
- Appearance check on trial parts (weld lines, sink, flow marks)
- Assembly check — every action cycled by hand and under power
- Final inspection before packing
Where Each Manufacturing Step Happens
| Step | Where it runs |
|---|---|
| Mold design (UG / NX + AutoCAD) | Tooling workshop |
| Steel selection & procurement | Tooling workshop, long-term suppliers |
| CNC rough & finish machining | Long-term partner shops, under our control |
| Sinker EDM | Tooling workshop |
| Wire EDM | Tooling workshop |
| Fitting | Tooling workshop |
| Polishing (up to optical polish) | Tooling workshop |
| Assembly | Tooling workshop |
| Trial molding (90T – 200T) | Tooling workshop |
| Inspection & CMM | Tooling workshop |
| Wooden case packing | Tooling workshop |
| Shipping & customs paperwork | Tooling workshop sales + long-term forwarder |